
Understanding Powder Coating Cure Times & Temperature Settings: A Powder Coater’s Guide to Getting Great Curing Results Every Time

This article will be most helpful for businesses using gas-fueled convection curing ovens in a batch curing setting. Gas-fueled convection ovens are the most popular ovens for professional powder coating situations. Conveyorized powder coating systems also typically use gas-powered ovens, but the dwell times are established by the conveyor rate. Although electric powder curing ovens are out there, and the information here applies to them as well, they tend to be much smaller in size and are primarily used by hobbyists.
Let’s Start by Identifying the 2 Most Common Powder Curing Problems:

Undercuring leads to soft (or sometimes brittle) film, poor adhesion, reduced chemical resistance, and early finish failure.

Overcuring is usually more forgiving. Most modern powders tolerate a moderate amount of extra time/temperature with only a mild change to the gloss or final color. Some white powders will “tell on you” by yellowing if they are exposed to excessive curing temps or dwell times. But, as a general rule, if you must choose, undercuring is worse than slight overbaking.
Next, Consider Your Powder Curing Oven’s Performance Characteristics

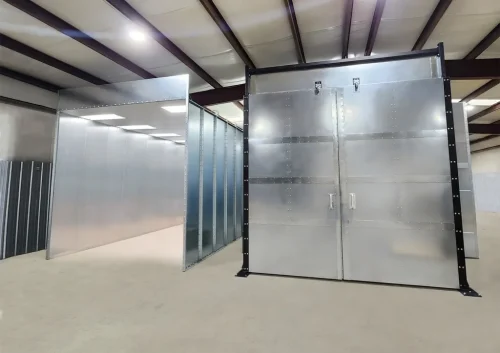
Powder curing ovens from reputable manufacturers like Reliant Finishing Systems provide excellent curing results because they heat the parts evenly and return to operating temps quickly when the doors are opened or the oven is shut down between batches. Look for models with thicker, better insulated wall and roof panels (6” is ideal), along with robust heat units with powerful recirculation fans.

Infrared (IR) ovens provide faster surface heating and work great for thin parts with simple geometries, such as panels and flat sheets, but they can create uneven surface temperatures on complex or dense parts if used as the only curing appliance. They are also typically much more expensive than convection curing ovens.
Although the most costly, hybrid ovens offer a nice mix of the performance benefits of both convection and infrared ovens. An IR section provides the initial heat-up of the powder (sometimes called the pre-gel phase), while also raising the temperature of the substrate. The convection section then evens out surface temps across the load and finishes the curing process.
IMPORTANT: Uniformity Trumps Frantic Speed (Think Slow is Smooth, and Smooth is Fast)
It’s tempting to focus on how fast your oven reaches setpoint and try to make every batch a race—especially in a busy job shop or heavy production environment—but ignoring load temps and secondary factors can be a costly mistake. Instead, focus on doing things the same way every time you deal with a similar load. Concentrate on getting uniform results, even if it takes a little longer.

This begins by understanding your oven’s capabilities and using them to best advantage. The oven can be fine-tuned during the initial set-up and calibration, and again whenever the oven is being periodically serviced. Some high-end oven companies, like Reliant Finishing Systems, send a technician to inspect the oven, start it up, calibrate it, and test its performance. They will even train your operators on how to operate and maintain the oven for best results. While on-site, techs will typically refine burner performance, verify temperature uniformity across the usable workspace, adjust recirculation airflow, tweak discharge duct output, and check for heat leakage. But their assistance doesn’t end once the oven is up and running. Reliant customers receive free lifetime phone support, including help troubleshooting temperature or tuning issues that may occur down the road when working with unusual parts or dealing with seasonal changes in the gas supply.
Once the oven is operating properly, it is important to keep burners, fans, ductwork, safety devices, and doors seals clean and well maintained. Spotty burner performance and improper airflow can cause inconsistent curing.
One of the most overlooked issues impacting both throughput and finish quality is “style of use.” Simply put, it means how you operate and maintain your equipment. A review of multiple shops doing similar work will typically reveal that some businesses get much better results from the exact same equipment.
There are obvious reasons why. Shops that take better care of their equipment have fewer unplanned oven shut-downs and less downtime overall. Along the same lines, shops that try to boost throughput by cutting dwell times short or running their oven at excessively high temps to shorten their curing routines often encounter higher reject rates due to curing issues.
Other problems may be less obvious. Some operators fail to maximize oven space by inefficiently racking their parts. A densely-packed oven may take longer to cure parts, but the difference is more than made up for by the increased number of parts being processed in each batch. Many operators fall into an inefficient rhythm of stopping and starting the oven because they don’t have enough parts staged and ready between cycles. Others dawdle while opening and closing the doors during loading/unloading, resulting in longer recovery times.
Probably the most prevalent style of use issue is the “one curing routine fits all” approach. Running every batch (regardless of batch size, part density, part complexity, or material) at a set time, like 20 minutes, and a set temp, like 400°F, is sure to lead to curing-related finish quality issues.

You Need to Understand What the Powder is Doing
Powder curing is a thermal-chemical process that involves 4 steps:
Step 1. Flow – The powder melts, flows together, and levels out.
Step 2. Gel – The viscosity rises as chemistry activates.
Step 3. Crosslink – The polymer network forms, locking in mechanical and chemical performance.
Step 4. Cool – Once the powder coating cools, usually within a few minutes, it is safe to handle lightly. What you may not realize is that some coatings can take several hours to reach their final hardness state, so don’t assume the powder coated part is ready for use as soon as it cools. Although the coating feels hard to the touch after it has cooled, the chemical reaction isn’t always complete when the part leaves the oven. The cross-linking continues at ambient temperatures, further strengthening the polymer matrix and increasing the coating’s hardness.
IMPORTANT: Curing Time Starts Once the Part Is Up to Curing Temperature
Starting your cure time when you finish loading parts into a hot oven is one of the most common mistakes powder coaters make. When your powder rep talks about the powder’s specs or technical data sheet (TDS)—also known as a product data sheet (PDS), and mentions “12 minutes at 400°F,” he means the part needs to stay at or above 400°F for 12 minutes AFTER the part metal temperature (PMT) reaches 400°F, NOT after the oven’s internal air temperature reaches 400°F.
Click here to see a typical PDS
What Does This Mean for Your Coating Operation?
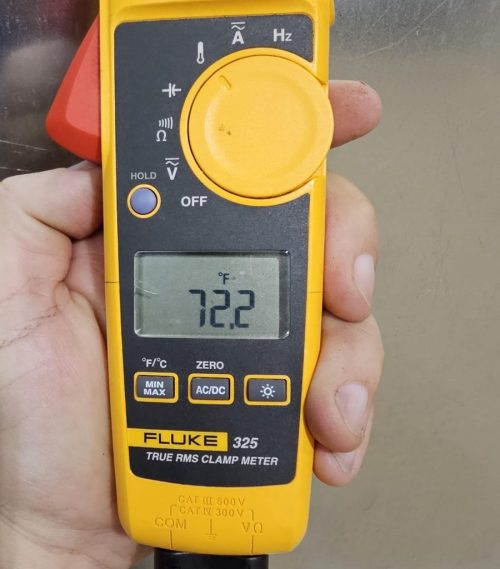
For best results, invest in a good quality temp probe system. It will include a temp probe (usually a type-K thermocouple) that connects to a handheld display or a heat-resistant data recorder. The probe is typically known as a bulb-type or contact thermocouple. It is meant to be attached (usually with tape or some type of clip) so the “bulb” or exposed metal tip is firmly touching the surface of the part. Fluke and other multimeter brands often have thermocouple attachments for their higher-end meters. You’ll probably need to get an optional extension wire so you can thread the probe wire through the oven door and attach it to the part.
Locate the portion of the part that is farthest from the heated air discharge points in your oven. If the part profile is complex, choose a spot that is blocked from direct air impingement, as this area will usually take longer to heat up. The goal is to monitor PMT at the coolest section of the part and time how long it takes to reach the desired curing temp. This will help you establish how long it takes for the part temp to ramp up to the desired curing temperature.
DON’T rely on a cheap handheld infrared “gun.” Imagine a cone-shaped area of sensitivity extending out of the front of the IR gun, sort of like the beam of a flashlight. Most of these devices have an effective range of only a few feet, and the farther the part is from the gun, the wider the “cone” of sensitivity is. So, you aren’t getting an accurate spot reading, you’re getting an average across the sensor’s detection area. Worse, the built-in laser only gives you an idea where the center of the detection cone is located. It doesn’t have anything to do with the reading–don’t think there’s anything fancy or technologically advanced about these products. They’re notoriously unreliable, especially if you’re dealing with a reflective surface or one that is heavily textured. Curved surfaces also frequently result in faulty readings. Don’t risk a lucrative project by relying on an $80 gadget.
How Does This Impact Cure Times in a Conventional Gas-Fueled Batch Oven?

Light, thin, small parts typically need 5-10 minutes to get to curing temperature.

Heavy, thick, complex, or densely racked parts can take 10-30 minutes to reach your target curing temperature. Extremely dense & complex parts, like large industrial machine parts, can require 30-40 minutes to reach curing temps—remember, you need to consider the coolest portion of the part, not the warmest.
Your total oven dwell time = ramp-up time + dwell time at specified PMT. For a fully loaded batch oven filled with moderately heavy parts, that usually means 25-45 minutes.
How Long Should I Cure a Powder Coated Part? What Temperature Should I Set My Oven To?
To answer these questions, you need to know what type of powder you’re working with. Here’s some typical curing schedules for popular powders, but you need to check the TDS for the exact powder you’re applying.
If you’re using a standard polyester powder, a common scheme is to cure for 10 minutes with a PMT of 400°. With higher durability polyesters, the temp range is about the same, but the dwell time can be up to 15 minutes. With low-temp polyesters, the curing temperature is lower, usually 325°–350°F, but the dwell time is longer, typically 20-25 minutes.
Urethane and hybrid powders are typically cured below 400° at 375°-390°F for around 10-12 minutes.
Epoxy powders cure at even lower temps, usually between 350°–375°F, but also normally require 10-12 minutes for best results.
How to Get Consistent Curing Results
For best results, you need to create unique curing routines (sometimes called schemes, recipes, or schedules) for parts of similar sizes, densities, and materials. We’ve already covered this in some detail above, but here’s a summary:
Use a temp probe to measure PMT. Attach the thermocouple to the slowest-to-heat section of the part.
Record ramp and dwell times. Log the time from oven entry to target PMT, then the dwell time at spec temperature.
Test your routine. Run multiple parts using the information you’ve compiled and check for a good cure.
Document your routine. Keep a simple instruction sheet for every group of similar parts. Record the oven setpoint, the expected ramp time, and the required dwell time at PMT. You can also use a sketch or written summary to describe parts/rack placement in the oven. Always include info from your QC checks.
Make good notes. Keep up with factors that can impact curing results. Are the racks extra-full, causing reduced parts spacing? Did you run a mix of aluminum and steel parts or light and heavy parts in the same batch? Did you encounter an oven shut-down or did someone fail to latch the doors properly? This information can help you keep track of potential issues. More sophisticated automated systems often include data logging controls, but you can do good job of keeping track of potential problems by using a notebook or marker board.
How to Avoid Common Powder Coating “Style of Use” Mistakes

We talked about style of use earlier, but let’s look at some of the most common operator errors that lead to curing defects.
Changing powders without re-profiling → Different formulations = different curing behaviors. Don’t guess, run a test.
Never running a test to begin with → Run a test with every new part family or load condition before you cure several batches. Don’t guess, run a test.
Failing to understand the performance of your oven → Work with a factory technician to map the oven or run performance tests with a Datapaq or similar data logger. Avoid hanging parts in areas with known temp extremes or understand how hotter or cooler areas will impact curing.

Ignoring part temp (PMT) → Measure your part temperature with a thermocouple during testing; don’t rely on the oven’s air temp display as a guide until you’ve at least done basic testing. Remember, most ovens use a single temp probe to measure the air temperature at only one point inside the oven. There can be significant temperature variations throughout the oven interior, especially with less expensive ovens.
Getting antsy and starting dwell time too early → Start dwell timing once you get the right PMT, not the moment you see the air temp return to setpoint.
Mixing heavy and light parts or steel and aluminum parts without a plan → Your curing routine needs to fully cure the most time-consuming parts without overcuring parts that reach curing temps more quickly. If you can’t safely do this, split the loads into separate batches.
Carelessly loading the oven → Tight spacing between parts restricts airflow, so you’ll probably need more time to get an acceptable cure with a heavily loaded rack. You may also need to change your curing routine if you’ve loaded the oven more densely than usual. DON’T block the intake for the heat system’s air recirculation fan(s) as this can significantly retard performance and/or cause shut-downs due to excessive heater output temps. If you load parts too closely to the oven’s hot air discharge ducts, you risk having powder blown off.
A Question We Get Asked All the Time: Can I Go Faster?
The answer is often YES, but it comes at a cost.
You need to stay within the powder supplier’s published guidelines, but most powders can be cured effectively using a handful of different temperature and dwell time combinations. These combos are based on a time vs. temperature equivalency. Typically, a shorter dwell time can be used if the curing temp (PMT) is higher. Higher oven temperatures can cause oven components to degrade more quickly, recovery times after opening and closing doors increase, plus you’ll burn more gas to reach those temperatures. Risks include gloss or color shifts and incomplete crosslinking if your curing routine is outside the validated range. Alternatively, you can select longer dwell times at slightly lower PMTs. Benefits to this strategy include energy savings and gentler heat on sensitive substrates. You should always confirm TDS guidelines and verify performance with data logging and QC tests before changing production recipes.
How to Confirm You’re Getting a Good Cure
Although you can use test panels (sometimes called witness panels or sample coupons) to confirm curing performance once you’ve established an effective curing routine, the best way to know you’re getting good curing results is to test a few parts that are then discarded or recoated.
You can use a data-logging system like an Elcometer or Datapaq to record actual PMT throughout the cycle and compare performance with the TDS guidelines. This is one of the best ways to ensure proper curing.
One of the fastest and least expensive ways to check for adhesion is to perform a cross-hatch test. This confirms that the finish has adequate bonding strength and hasn’t been undercured.
You can also perform a solvent rub test, which is usually done with MEK. This is a fast way to check the coating for crosslink performance (and confirm solvent resistance).
You can learn more about QC testing by clicking here.
Some coaters like to make sure the powder they’re using doesn’t have any defects and confirm there wasn’t an unseen hiccup with the curing process. They do this by including test panels with every load and checking them for discoloration and other finish flaws before bending them to see if there is unusual delamination or cracking of the coating.
Want to Learn More?
Have powder coating questions or want to discuss powder coating equipment? Give the experts at Reliant Finishing Systems a call at (256) 355-9000 or click here for an easy-to-use online contact form.