
Poor Process Balance: The Overlooked Powder Coating Problem
For all powder coaters, especially larger industrial powder coating operations, the most expensive problems are not always caused by bad powder, poor equipment, or careless employees. Instead, their coating line’s effectiveness may be getting clobbered by something less obvious. Whether using a batch or conveyorized powder coating system, the real issue in many facilities is process imbalance. The pretreatment system, dry-off oven, powder booth, application equipment, conveyor/cart movement, and curing oven may all function individually at what seems like an acceptable level, but they may not function well when viewed as a coordinated production system.
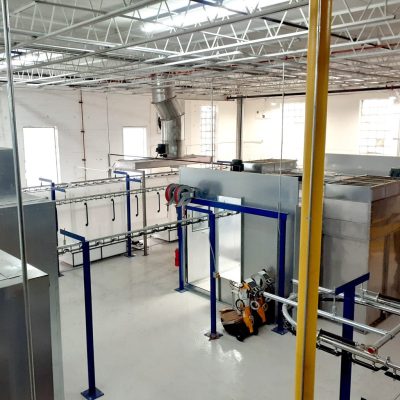
That distinction matters because small issues throughout the coating process become roadblocks to profitability once they pile up. A successful powder coating operation is more than just a group of machines and operators. It should be a controlled manufacturing process. When one phase of the process is poorly maintained, log-jammed/undersized, improperly adjusted, or out of sync with the rest of the process, the entire operation suffers. The results usually show up as slow throughput, excess labor, wasted powder, substantial rework, inconsistent film thickness, poor adhesion, unusually long cure windows, or operators making constant adjustments to compensate for system-level problems.
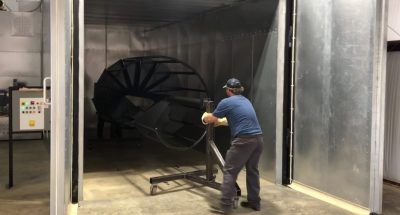
Bart Roegner, CEO of Reliant Finishing Systems, observes, “A fair amount of our business comes from companies that already know powder coating, but still can’t get their finishing line to produce the results they need. Sometimes the problem is obvious. A worn-out multi-stage washer. An oven that was never built for the current workload. A line that has been pushed past what it can reasonably do. Other times, it is not one big failure. It is ten smaller failures stacked on top of each other until the whole system starts failing. Those are the jobs we like. We can step back and look at the coating operation as a system. We are not buried in the day-to-day frustration. We are not worn down by the same recurring problems. We can see the line clearly, identify what is actually driving the failures, and apply experience the customer may not have internally. That is one of Reliant’s real strengths: we solve system-level finishing problems without overcomplicating things.”
Let’s move through the finishing process step-by-step to identify potential areas of concern, starting with parts prep. The vast majority of finish defects are caused by improper parts preparation. Pretreatment should always be evaluated as a component of the full coating process, even if it takes place elsewhere (such as when parts are blasted off-site before being coating). A well-designed pretreatment process removes soils, improves surface condition, and supports adhesion and corrosion resistance. However, if parts leave pretreatment with blasting debris, trapped moisture, chemical residue, or inconsistent surface preparation, the other equipment in the process can’t fix these problems. That’s why it is critical to routinely review chemical concentration, rinse quality, water condition, nozzle performance, dwell time, and dry-off effectiveness for chemical pretreatment systems, and blast nozzle wear, compressed air quality, and blasting media choices when mechanical surface preparation is required.
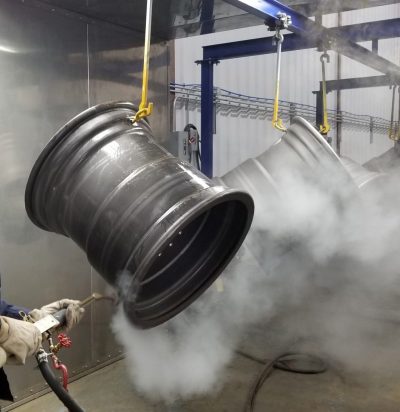
Once pretreatment performance has been reviewed, including the performance of the dry-off oven if one is in use, the next step is to consider the powder coating booth and what takes place inside it. There’s a lot that can go wrong without giving immediate warnings.
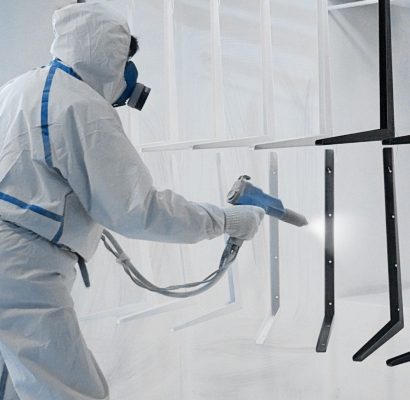
As an example, coating inefficiencies aren’t always glaringly obvious. First-pass transfer efficiency is one of the most important metrics you can measure. In a larger industrial setting, even a modest improvement can have a major financial impact. If a plant applies hundreds of pounds of powder per week, improving transfer efficiency by only 10% can reduce powder waste, coating time, filter maintenance, reclaim handling, and cleanup time. Better transfer efficiency also tends to improve consistency because operators aren’t fighting the system to get adequate coverage.
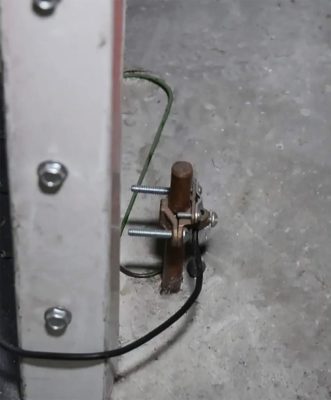
Grounding is a related issue that deserves regular attention. Poor grounding reduces powder attraction and makes it harder to coat quickly and efficiently. Hooks, racks, carts, conveyor components, and other contact points should be inspected periodically for powder build-up. A part that appears to be grounded because it’s hanging from grounded equipment may still have a poor ground path if the contact surfaces are insulated by coating residue. In addition to clean contact points for parts, it’s not uncommon for supplemental grounding to be necessary for achieving optimal results. This is often done using copper grounding rods and heavy gauge grounding straps at the booth. In all coating operations, especially ones that routinely see a large volume of parts traffic, grounding should be treated as a high-value maintenance item, not a one-time setup detail.
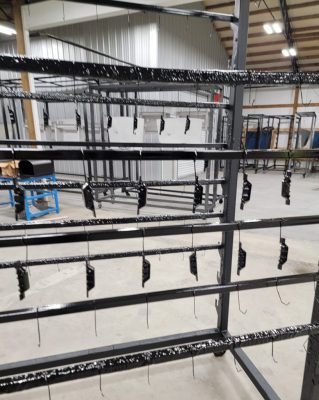
Parts orientation and hanging schemes are also important. Some coaters, especially fabrication job shops and powder coating service providers, process a wide mix of parts. Inconsistent loading patterns can create inconsistent results. If parts are hung too close together, airflow and powder cloud movement may be restricted. If parts are oriented poorly, painters may have to over-apply powder to reach hidden surfaces or reposition carts by hand to gain access. Better organized racking and spacing can improve finish quality without changing the powder or the equipment.
Another common issue is poor airflow balance in the powder booth. Industrial powder booths must capture overspray effectively, but excessive airflow can pull charged powder away from the parts before it has a chance to adhere. This is most common in undersized booths, where the displacement caused by the load leads to excessive air velocity around the part. The same thing can happen if a portion of the load is too close to the exhaust filter surface. When these issues occur, first-pass transfer efficiency drops. The booth interior may look fairly clean, and the exhaust system may appear to be working well, but the company is spending more on powder, filters, and labor than necessary.
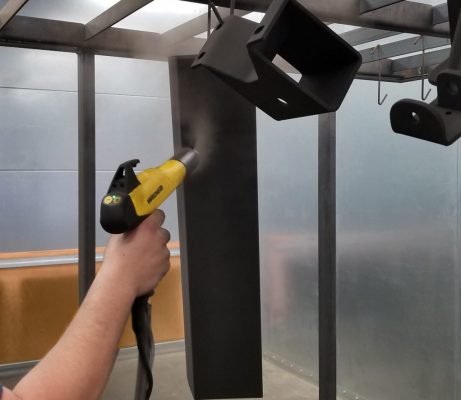
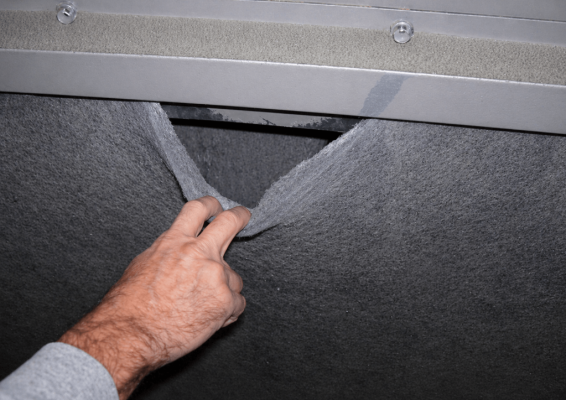
At the other extreme, some booths have inadequate airflow, often due to clogged filters. In fact, poor filter maintenance is probably the number one cause of powder booth performance issues. Insufficient airflow can cause the powder cloud to hang in the air around the part after an appropriate amount of powder has already coated the surface. The painters must deal with decreased visibility, which can lead to errors. The powder overspray eventually falls to the floor in the workspace without being moved towards the exhaust. The painters end up dealing with a heavy film of powder underfoot, which can be a safety issue, plus the wheels on rolling racks get soiled with powder build-up more quickly. This situation necessitates increased booth cleaning labor and can also lead to incidental cross-contamination issues when changing between powders during the workday.
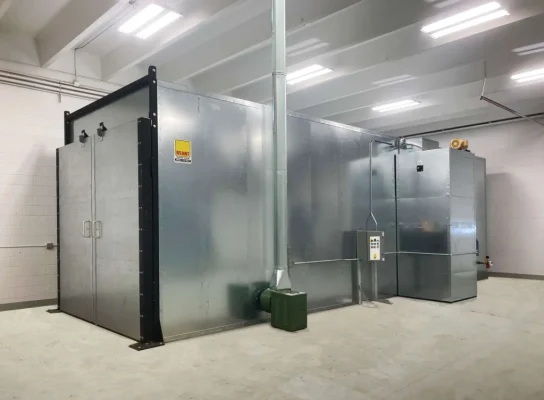
Similarly, airflow issues inside the curing oven can limit productivity. A powder curing oven needs adequate, evenly distributed heated air across the entire work envelope. If airflow is weak, uneven, or blocked by poor part spacing, some areas of the load may reach cure temperature much later than others. Operators may respond by increasing dwell time or raising the setpoint. That may help the worst-case part cure properly, but it can also increase fuel consumption, slow production, and risk overbaking lighter or thinner parts. If heavy parts and light parts are mixed without considering cure response, some parts may be under-cured while others are exposed to unnecessary heat.
Even with ovens that are designed with a substantial work envelope where temperatures are relatively uniform and airflow is appropriate, poor hanging practices can lead to problems. This is most commonly found in batch coating situations where managers are pushing for maximum throughput or employees haven’t been properly trained. Operators end up racking parts well outside the oven manufacturer’s designated curing envelope. This happens by jamming parts against the discharge points of the oven’s heat system or hanging them too close to the floor or doors. The parts end up being blasted by hot air that hasn’t had a chance to normalize across the curing zone or located in an area inside the oven that will never have adequate curing performance.
As mentioned earlier, finishing operations should evaluate powder coating performance as a complete process instead of troubleshooting each defect in isolation. For example, adhesion failure may be blamed on the powder or the curing routine, but the root cause could be poor pretreatment. Surface defects like orange peel may be blamed on the gun settings, but the real problem may be that the parts are too hot coming out of the drying oven, taking too long to get to temp in the curing oven, or you’re dealing with excessive film build caused by repeated touch-up. Color inconsistency, particularly with whites and light colors, may be blamed on the supplier, while the actual cause may be inconsistent cure temperature or contaminated reclaim powder.
Bart Roegner adds, “A useful starting point is to measure the entire coating process in practical terms. You may find that easier and more useful than trying to drill down on the technical aspects right away. It’s rare that you can fix everything all at once, so after you get an objective look at the big picture, you can prioritize your efforts.”
Typical questions might include:
How many different parts are coated in a typical day/week/month and what size are they?
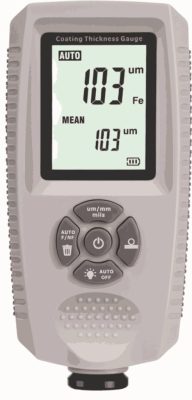
What is the target film thickness and what’s currently being achieved?
How many pounds of powder are purchased versus how many pounds are actually deposited on saleable parts? Has this shifted when changing powder vendors or using different products?
How often are parts recoated or touched up? Are the types of failures recorded and tallied?
How many operators are needed at each stage of the process to get maximum productivity? How many do we have now?
How much time is lost each day/week/month waiting on pretreatment, drying, booth availability, or oven capacity? Is there a log showing what phases of the process caused delays?
How much time is lost each day/week/month due to unplanned equipment downtime? Is there a log of what appliances were down and why?
Getting answers to these questions can reveal whether the current coating operation is an effective production asset or an ongoing fight against bottlenecks, waste, and defects. If these answers aren’t immediately available, a good first step (if you’re not dealing with an emergency due to powder coating issues at your facility) would be to put systems in place so you can get the information you need to make objective decisions.
The best powder coating systems are designed around the work being processed. Part size, material thickness, production volume, coating specification, available labor, floor space, handling method, and future growth plans all affect equipment selection. A booth, oven, washer, or conveyor that looks adequate on paper may not deliver the desired output if the full operating pattern is not considered.
This is where experienced system design matters. Reliant Finishing Systems works with manufacturers, fabricators, and coating operations that need practical, dependable powder coating equipment built around real production requirements. For industrial coating operations of all sizes, the goal should not be to simply to buy an adequately sized equipment package. The goal should be to create a balanced coating process that maximizes throughput, reduces waste, supports consistent quality, and gives the company room to grow.
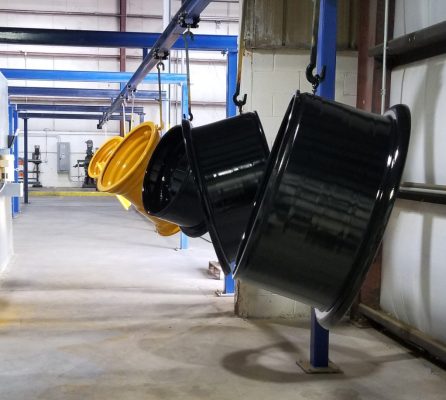
A well-balanced powder coating operation does not depend on constant operator correction by experienced, highly skilled employees. It gives even inexperienced, moderately skilled operators the right conditions to succeed. Airflow, heat, grounding, pretreatment, part movement, and application technique all work together. When those elements are properly matched, the result is lower operating cost, better finish quality, fewer rejects, and a more profitable coating department.
Want to talk with an expert about your coating operation? Give Reliant Finishing Systems a call at (256) 355-9000 or click HERE. Check out our website at www.reliantfinishingsystems.com.