Outgassing: A Practical Guide for Powder Coaters

Michael Schuerer
President, Reliant Finishing Systems
This guide is intended for powder coaters, finishing department managers, and powder coating shop owners and managers. It addresses outgassing in a practical way and explains pragmatic methods to deal with it and the finish defects it can cause. It relies on the technical expertise and field experience of coating equipment specialists like Reliant Finishing Systems, as well as other coating experts, pretreatment chemical providers, and leading powder suppliers.
Unfortunately, there are a number of online resources created using AI that provide contradictory information or suggest approaches that are not practical for a working shop. Use caution when considering online guides, especially those that appear to have been created almost entirely using AI.

What is outgassing and why is it a finishing problem?
Outgassing-related finish defects are one of the most persistent appearance problems encountered when powder coating cast parts, galvanized steel parts, assemblies that include cast aluminum or zinc components, and some welded steel parts. Air, moisture, casting lubricants, trapped pretreatment solution, or other volatile material can escape from pores or tiny gaps in the substrate during the powder curing process and pass through the molten powder film. If the film has already started to gel, the escaping gas can leave pinholes, bubbles, craters, or even large blisters.
This differs from ordinary surface contamination, although inadequate cleaning during chemical pretreatment may produce nearly identical defects. Although other metal parts can exhibit finish defects from outgassing, castings are particularly vulnerable because porosity can extend from the interior of the part to the surface, where it can retain air and process-related contaminants.
A practical diagnostic guide for determining if outgassing is the root cause of a finish defect
In busy powder coating operations, many defects blamed on outgassing are actually due to either a) contamination that hasn’t been fully removed by cleaning or b) trapped-liquid release linked to poor drainage/insufficient drying. The location of the defect is usually the best clue for determining the cause. Before adding a process like high temperature pre-baking to address outgassing, locate where the defect occurs and investigate what material could be trapped at that location. This often produces a less expensive and more reliable correction than assuming every rejected part needs outgassing.


How do you get better finishing results with cast parts?
The first control point is the casting itself. Parts with dense, sound cast structure are much easier to finish than castings containing interconnected porosity, shrinkage cavities, or poorly vented sections. Your powder coating department may have little leverage over the casting process, but it should still identify recurring failures by department/supplier and production lot. Outgassing defects that repeatedly appear in the same area of the same part are often a casting quality or geometry problem rather than a coating line problem. Addressing these issues with the production manager or vendor may lead to corrective discussions about metal temperature, mold venting, release-agent use, fill rate, and pressure or vacuum practices.

If you’re going to use other methods to reduce outgassing defects, how important is chemical pretreatment?
Chemical pretreatment remains necessary because pre-baking does not replace cleaning or the use of a conversion coating. A typical pretreatment process may include alkaline degreasing, rinsing, etching or deoxidizing where required, conversion coating, final rinsing, and drying. Parts require particular attention to blind holes, recesses, threaded cavities, lap joints, and upward-facing pockets that can retain chemicals or rinse water. Racking should promote complete drainage when practical. Even when using an otherwise fully effective drying oven, compressed air blow-off may be justified for difficult geometries. Hidden oils, moisture, accumulated pretreatment chemistry, and other contaminants can lead to defects during powder curing. A “clean-looking” part is not necessarily a fully dry and stable part ready for the application of powder.

How do you process parts by pre-baking to reduce outgassing defects?
The most reliable in-house treatment to minimize coating defects related to outgassing is a controlled heating process typically called “pre-baking.” The objective is to bring the part-metal temperature above the temperature the parts will experience during powder curing and hold it long enough for volatile material to escape. Most experts have similar but slightly different advice: temp recommendations range from approximately 20°F above the normal cure temperature up to about 80°F above the specified part-metal temperature that will be reached during powder curing. This is a good range to use during in-house testing rather than a hard-and-fast rule.

A digital temperature meter that uses a thermocouple or a temperature profiling instrument known as a data logger should be used to measure the heaviest and most shielded sections of the parts because the oven’s air temperature display does not establish whether the part itself has reached the target temp in a given dwell time. DO NOT use a contactless “temp gun” to determine parts temperature—they’re notoriously inaccurate at higher temps or when measuring part temps at a distance, making them undependable in powder coating settings. If you don’t have a way to precisely measure peak part temperatures, it may be best to err on the side of caution and give the parts extra time beyond your initial dwell time estimate.
A general dwell time range is no less than 20 minutes and no more than 60 minutes AFTER the desired part-metal temp is reached. The dwell time depends on the substrate material, as well as the part density and complexity.
Don’t let perfect be the enemy of good! In many shops, the best that can be hoped for is to use the same set point and dwell time for the pre-bake cycle that’s used for the curing cycle. Although this will yield less-than-ideal results, testing will probably show that the number of outgassing-related defects can be reduced using this approach.

Should I pretreat the parts before or after heating them to address outgassing?
Deciding when to pre-bake parts can be tricky. If using a pretreatment chemical that combines a degreaser and a conversion coating, you may have only one option: to pre-bake the parts after they have been prepped chemically. When parts have been pretreated with chemicals before being thermally processed, the pretreatment supplier should approve the proposed pre-bake temperature and exposure time. The required outgassing temperature and time must be established experimentally because conversion-coating chemistry, part mass, porosity, storage history, and final performance requirements all affect the result.
When severe outgassing makes a pretreat-first sequence unreliable, the more effective route is often initial degreasing, prebaking the bare part, and then performing the final chemical pretreatment and dry-off or secondary baking immediately before powder application.
When using a conveyorized coating line, that sequence may be impractical or unachievable. To get satisfactory results, it may be necessary to use the dry-off oven as a moderate outgassing stage by increasing drying temperature and dwell time (this usually means slowing the conveyor significantly). Pre-baking parts using a separate batch oven may be the most workable solution. Once you’ve modified the process, it should be tested by checking adhesion, finish appearance, and corrosion resistance rather than assumed to be satisfactory.
Parts should normally be coated soon after pre-baking. A slightly warm casting is desirable because prolonged storage allows porous metal to reabsorb humidity and air. The part should not be so hot that powder melts on contact and builds excessive film or becomes difficult to apply uniformly. A practical target for part temp is often approximately 25–30°F above ambient while spraying, followed by curing according to the powder supplier’s part-metal schedule.

Does the powder I use matter?
Careful powder selection can materially improve your results. Outgassing-forgiving powders and anti-gas primers are formulated to keep the film sufficiently open or fluid for gas to escape and the surface to reflow. They reduce minor defects but do not usually make a contaminated or highly porous casting acceptable. Powders that cure at lower temps are also useful, especially for zinc die castings. The International Zinc Association recommends keeping zinc-alloy die castings at or below approximately 338°F when possible because higher temperatures substantially increase blistering risk. That’s why you sometimes see powders that have a baseline cure time listed at 338°F and a shorter cure time listed at a higher temp, such as 392°F. Low-cure polyester or hybrid powder systems can provide a practical advantage if the final finish has been tested and proven to provide adequate performance.
Film thickness must be more carefully controlled when dealing with problematic parts. Heavy powder deposition can skin over before the gas has escaped and can turn an otherwise acceptable part into a reject. Apply within the powder manufacturer’s recommended range, with special attention to edges, recesses, and electrostatic wrap areas where excessive build may occur. A two-coat system using an anti-gas primer can be effective for some parts, but the total film build and intercoat cure schedule must be qualified.
Re-coating parts rejected due to outgassing-related defects rarely works without stripping them. Simply adding more powder to hide pinholes can make the situation worse by exaggerating defects rather than masking them as intended.

Are there any workarounds worth trying in an urgent situation like a rush job?
Bart Roegner, CEO of Reliant Finishing Systems, has encountered a technique commonly called hot flocking. In this approach, a properly pretreated and fully dried part is heated to an elevated part-metal temperature before powder is applied. The exact temperature must be selected based on the substrate, pretreatment system, and the powder manufacturer’s published cure schedule, but the part may be heated to approximately 400°F for some applications.
The part is moved to the powder booth and given a light initial coat while it is still hot. The powder melts and begins to flow almost immediately upon contacting the surface. The part is then allowed to cool enough for the remaining powder to be applied until the desired film thickness is reached. It is returned to the oven and cured according to the powder manufacturer’s recommended time at part-metal temperature.
Some customers have reported that this process can reduce visible outgassing defects on difficult castings or other porous substrates. The exact reason it works may vary depending on the substrate, the contaminants present, the powder formulation, the temperature profile, and the timing of application. It should therefore be treated as a practical application technique rather than a guaranteed solution.
Hot flocking requires a skilled painter and generally involves some trial and error using test parts. Applying too much powder during the first pass can create excessive film build, sagging, orange peel, or other appearance problems. Particularly troublesome parts may still require a separate pre-bake or degassing cycle before pretreatment and coating.
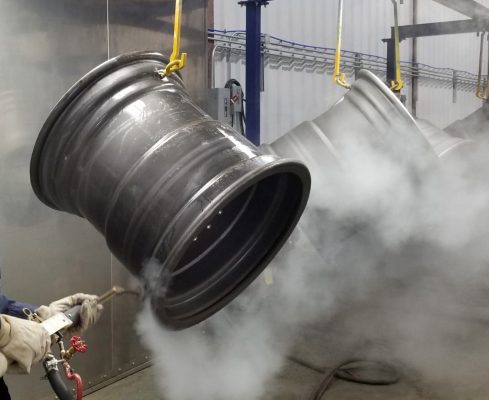
Because the process is labor intensive and difficult to control consistently, it is generally better suited to small quantities of difficult parts, although some alloy wheel manufacturers have successfully automated this process and get good to great results.
Also, It is important not to confuse this technique with the hot application processes used to coat electrical bus bars. Although both methods involve applying powder to a heated metal part, they are fundamentally different applications. In the process described above, conventional powder is applied with an electrostatic spray gun in an effort to reduce visible outgassing defects on a limited number of troublesome parts. Electrical bus bar coating on the other hand; utilizes specialty powders, very specific fluidized-bed application, and a tight cure schedule. This results in a repeatable process that can be automated and scaled for very high throughput.

How Do I Bridge the Gap Between Best Practices & Profitability?
An ideal process would involve pre-baking every questionable part, profiling every different load scheme with a data logger and adopting an ideal prep, coating, and curing routine, using a dedicated outgassing-resistant powder/primer, and holding all parts in a climate-controlled staging area only very briefly before powder application. Most job shops and busy finishing departments cannot do all of this.
A pragmatic solution involves a finishing program that classifies parts by risk. New castings, oily or previously used cast parts, aluminum parts with unusually heavy sections, previously rejected parts, zinc die castings, and lots that include parts with a history of pinholing receive a pre-bake and test coat. Stable parts from proven suppliers may run through the normal pretreatment and dry-off process. Problem parts can be scheduled together for “batch” pre-baking, minimizing disruption to the main line. Records should include info about the supplier, lot, pretreatment parameters, pre-bake part temperature and hold time, powder code, film thickness, and defect rate. Testing several pieces before committing an entire production load is particularly important with an unfamiliar casting or potentially problematic part.
Finally, acceptance standards should match the part’s function. A decorative consumer component may require a nearly flawless surface, while a concealed industrial casting may tolerate isolated microscopic pinholes if adhesion and corrosion resistance remain adequate. The coating manager should establish the appearance requirement and rejection threshold before committing to costly special processing.
The practical goal is not the elimination of every pore-related defect, it is to achieve a repeatable combination of suitable powder use, adequate cleaning, thorough drying, controlled heating during pre-baking and curing, and realistic inspection criteria—all at an economically defensible cost.
Michael Schuerer is the founder and president of Reliant Finishing Systems. He entered the finishing industry in 1999 and founded Reliant in 2005. He has visited hundreds of manufacturing facilities to evaluate process requirements, discuss finishing equipment, and troubleshoot operational issues. He also regularly contributes to technical articles on industrial finishing and thermal processing applications.